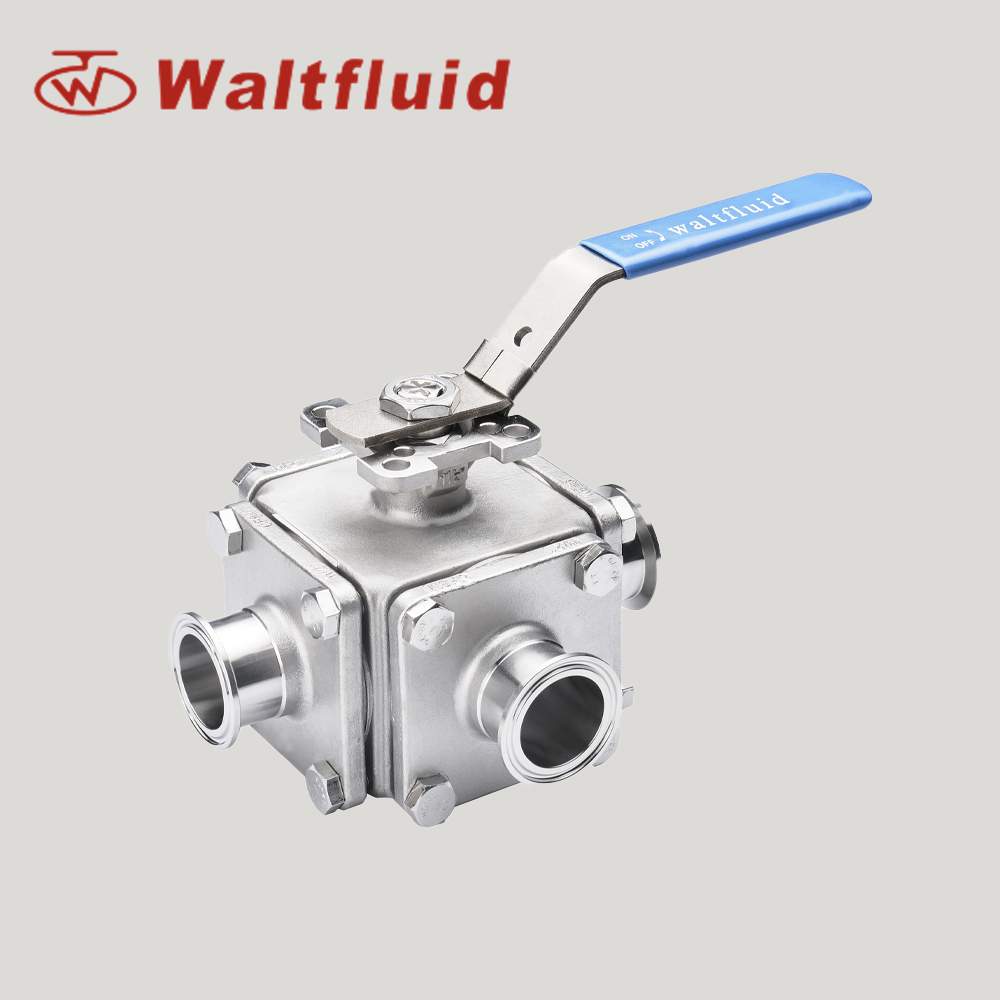
**Innovative Ball Valve With Drain Enhances Industrial Fluid Control Solutions**In today’s fast-evolving industrial landscape, efficient fluid management systems are critical for ensuring operational excellence and environmental compliance. A notable advancement in this area is the introduction of the new Ball Valve With Drain, a product designed to streamline fluid control with enhanced safety, reliability, and maintenance ease. This development aligns with the company’s commitment to providing superior industrial components that meet the rigorous demands of modern industries.### Product Overview: Ball Valve With DrainThe Ball Valve With Drain is engineered to offer precise flow control alongside an integrated drainage capability, setting it apart from conventional ball valves. This dual functionality allows for not only the regulation of fluid passage but also the ability to safely discharge any residual liquid, ensuring minimal contamination and reducing downtime during maintenance.Constructed from high-grade materials, the valve demonstrates exceptional resistance to corrosion, pressure, and temperature variations, making it suitable for a broad range of applications. Industrial sectors such as chemical processing, oil and gas, water treatment, and manufacturing stand to benefit significantly from this innovation.### Key Features and Benefits**1. Integrated Drainage System:** The defining feature of this ball valve is its built-in drain, which facilitates the removal of trapped fluids without needing to dismantle the entire valve assembly. This design ensures safer handling of hazardous substances and promotes easier and faster system flushing.**2. Enhanced Safety Measures:** By enabling controlled drainage, the valve reduces the risk of accidental spills and exposure to harmful fluids, protecting personnel and the environment. The robust sealing mechanisms further prevent leaks, ensuring operational integrity.**3. Durability and Longevity:** Manufactured using premium materials that resist wear and chemical attack, the valve maintains optimal performance over extended periods, even under harsh operating conditions. This durability translates into lower replacement costs and higher uptime.**4. Simplified Maintenance:** The drain feature drastically simplifies valve servicing, allowing technicians to quickly and efficiently remove residual fluids before disassembly. This minimizes system downtime and maintenance labor costs.**5. Versatile Application Range:** Thanks to its adaptable design, the valve fits seamlessly into various piping systems and is compatible with different fluid types, including aggressive chemicals, gases, and liquids. Its customizable options allow it to meet specific client requirements.### Company Commitment to Innovation and QualityThe company behind the Ball Valve With Drain has established a reputation for delivering cutting-edge solutions tailored to the needs of industrial clients worldwide. With decades of experience in valve manufacturing and fluid control technology, the company emphasizes research and development, quality assurance, and customer service.Their manufacturing facilities employ state-of-the-art processes and undergo rigorous quality inspection protocols to ensure that every valve meets international standards such as ISO and API certifications. This commitment guarantees products with consistent performance and reliability.Furthermore, the company provides comprehensive technical support, assisting clients from product selection through installation and after-sales service. This holistic approach contributes to building long-term partnerships and advancing industry standards.### Industry Impact and Customer FeedbackSince its market introduction, the Ball Valve With Drain has garnered positive feedback from multiple sectors. Users report significant improvements in safety procedures and maintenance efficiency, translating into cost savings and smoother operational workflows.One customer in the chemical processing industry noted, “The integrated drain has transformed our maintenance routines, allowing us to handle hazardous liquids with greater confidence and less downtime.” Similarly, a water treatment plant manager highlighted the valve's durability and ease of installation as critical factors in their decision to adopt it across various sites.These testimonials underscore the valve’s practical advantages and reinforce its position as a valuable addition to fluid management systems.### Future Prospects and DevelopmentsLooking ahead, the company plans to expand the Ball Valve With Drain’s offerings by incorporating smart technology features such as remote monitoring and automated control. These enhancements aim to provide real-time data on valve status, fluid flow, and potential leakages, thereby further improving safety and operational efficiency.Additionally, efforts are underway to develop environmentally friendly variants utilizing sustainable materials and designs that align with global green initiatives.### ConclusionThe Ball Valve With Drain represents a significant leap forward in fluid control technology, merging functionality, safety, and durability in a single product. As industries continue to prioritize efficiency and environmental responsibility, such innovations are vital in meeting these evolving challenges.Backed by a company renowned for quality and innovation, this valve is set to become a standard in various industrial applications, supporting safer, more efficient, and cost-effective operations. Organizations seeking reliable fluid management solutions will find this product an invaluable asset in their infrastructure, reinforcing their commitment to operational excellence and sustainability.
Read More